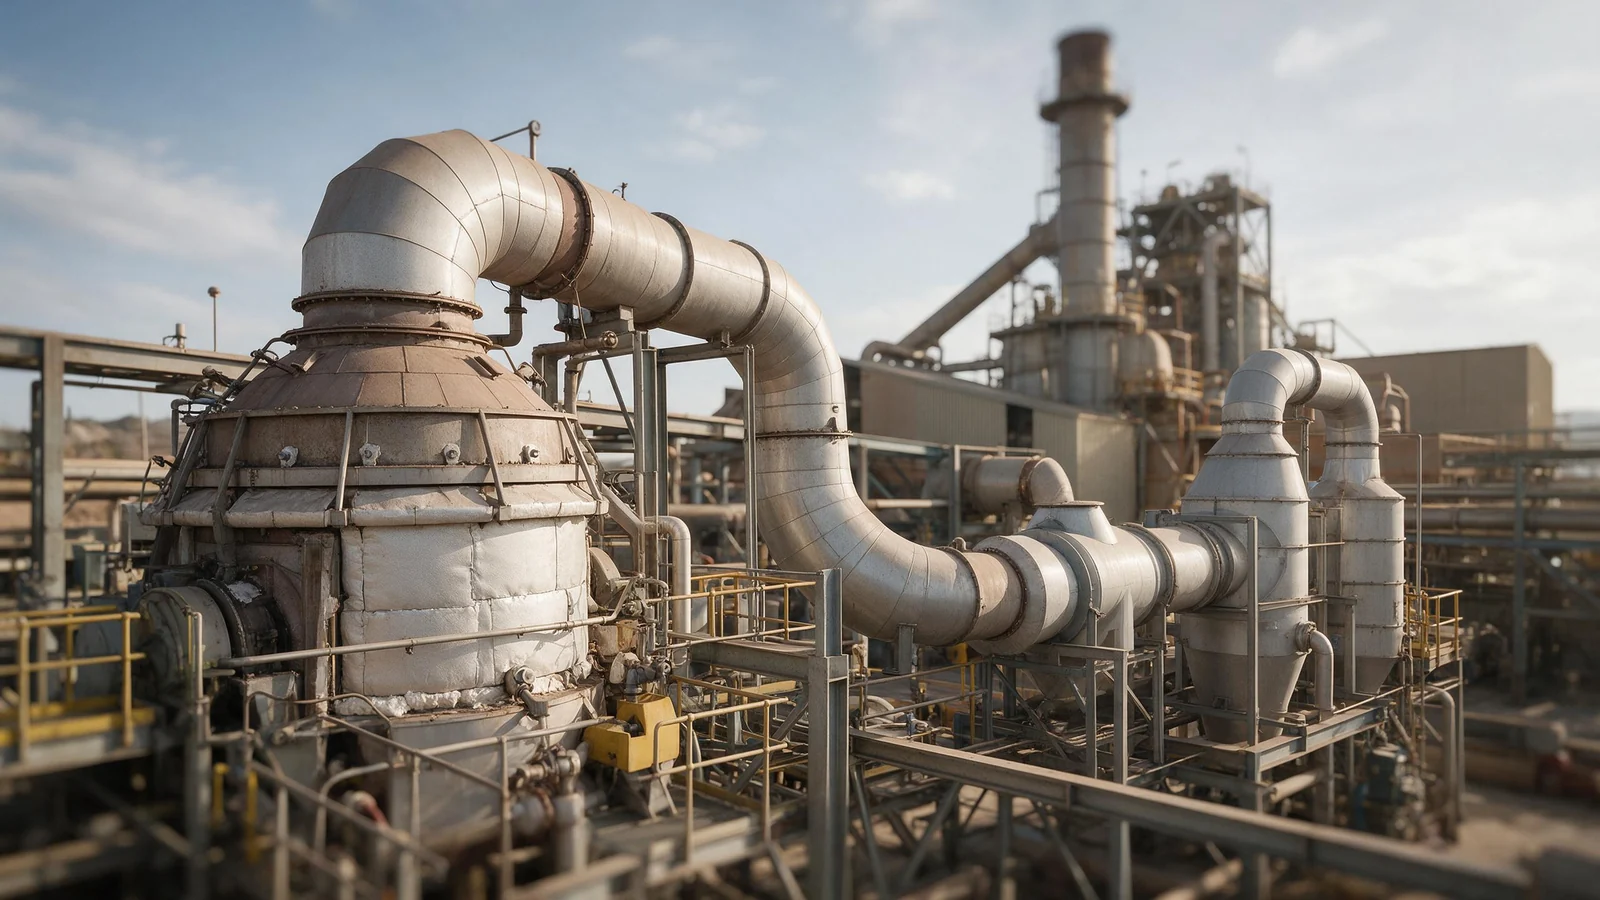
Say a mine owner asks how to handle a refractory gold ore that won't respond to direct cyanidation. My first question is always the same. How much gold is locked in sulphides? And how much is stolen by carbon? Gold roasting is one answer, but not a universal one. It's an oxidative pretreatment. Nothing more.
Why refractory gold ore needs roasting
A refractory gold ore is one where direct cyanidation recovers too little gold. That's the whole definition. The gold sits locked inside sulphide minerals. Usually pyrite or arsenopyrite. The cyanide can't reach it. It's stuck. In a double-refractory ore, you get another problem. Naturally occurring carbonaceous matter adsorbs any gold that does dissolve. It's greedy. That's preg-robbing. You leach the gold out of one mineral. Then the carbon grabs it before you can recover it. Roasting attacks both problems. Before leaching.
The mechanism matters. Let's look closer. Sulphide minerals act as a shell. A hard one. As long as the shell is intact, the leach solution can't get to the gold inside. It just can't. Carbonaceous matter behaves like activated carbon in a CIL circuit. Same idea. It steals gold cyanide complex out of solution. Straight out. A roasting step changes both materials at once. One step. That's why it suits double-refractory ores. It's a two-for-one.
You can read more about the chemistry of refractory gold in metallurgical testwork for gold ores, and the downstream leaching step is covered in gold leaching. Just hold on to this. Roasting is not a recovery process. It's a liberation step. That's the key.
What roasting does to sulphides and carbon
Roasting heats the ore in an oxidising atmosphere. Simple start. Sulphide minerals like pyrite and arsenopyrite react with oxygen. They burn. You drive off sulphur as sulphur dioxide. You leave behind porous iron oxides. The porosity is the point. Remember that. A roasted particle is full of tiny channels. Thousands of them. They let cyanide reach the gold. Finally. The U.S. EPA describes this transformation clearly: with an oxygen-containing gas, sulphides of iron, zinc, copper and other metals turn into solid oxides or sulphates and gaseous sulphur dioxide at elevated temperatures, reported in the range of 400 to 800 degrees Celsius (EPA HERO).
Carbon is another matter. It's trickier. Organic carbon in the ore, the preg-robbing kind, burns off as carbon dioxide. Gone. That stops the carbon from adsorbing dissolved gold later. Problem solved. What remains is called calcine. Know that term. Its structure controls how well the subsequent cyanidation works. It's that important. If the calcine is too dense or too sintered, recovery suffers. Badly. So roasting temperature, oxygen level and residence time are operating variables. Not fixed settings.
One laboratory study on a Carlin Trend ore gives a useful reference point. It's a good data point. Under defined roasting conditions, including a top particle size of 150 micrometres, the maximum gold extraction was 92 per cent, with a head grade of 5.7 grams per tonne and leach residue of 0.4 grams per tonne (EPA HERO). That's one ore. Not a promise for yours.
Roasting compared with other pretreatment routes
Route selection is not a beauty contest. It's engineering. Each option has a cost, a timeline and an environmental footprint. All three matter. Those shift with the ore. Every ore is different. The table below is a starting point. Not a decision matrix.
| Route | What it does | Where it tends to fit | Main limit |
|---|---|---|---|
| Roasting | Oxidises sulphides at elevated temperature to porous oxides; burns off carbonaceous matter | Double-refractory ores with both sulphide locking and preg-robbing carbon | Off-gas handling for sulphur dioxide, arsenic and mercury |
| Pressure oxidation (POX) | Oxidises sulphides in an autoclave under oxygen pressure and high temperature | Refractory sulphide ores where arsenic deportment is manageable | High capital intensity and acid generation |
| Bio-oxidation | Uses bacteria to oxidise sulphide minerals over days or weeks | Low-grade sulphide ores with a long project timeline | Slow kinetics and sensitivity to temperature and toxins |
| Ultrafine grinding | Reduces particle size to expose more gold to cyanide | Sulphide ores where gold is finely disseminated but carbon is not preg-robbing | Does not remove carbon or oxidise sulphides |
Pressure oxidation handles sulphides well. But it doesn't burn off preg-robbing carbon. Bio-oxidation can be gentler on capital. But it is slow. Very slow. Ultrafine grinding is cheaper to implement. True. Yet it only exposes gold. That's all. It doesn't change the chemistry of the host mineral. No reaction. If your ore is double-refractory, roasting often wins. Often. It attacks both the sulphide shell and the carbon thief. One step.
Off-gas, arsenic and environmental controls
You can't discuss roasting without discussing the gas leaving the roaster. It's unavoidable. Sulphide oxidation produces sulphur dioxide. That gas is toxic and regulated. The U.S. OSHA general industry permissible exposure limit for sulphur dioxide is 5 parts per million, or 13 milligrams per cubic metre (OSHA method 1011). A plant must keep stack emissions and workplace exposure well inside that line. Well inside. That means scrubbers, gas cooling and particulate collection. All of it.
Arsenic makes the gas cleaning harder. A lot harder. If the ore contains arsenopyrite, roasting volatilises arsenic as arsenic trioxide. That's a fact. That compound must be captured, usually as a dust. Before it escapes. Mercury, where present, behaves similarly. Same problem. The off-gas train is not an add-on. Never think that. It shapes the plant layout, the materials of construction and the operating permit. Everything. If you're comparing suppliers, ask them to explain the gas cleaning sequence in detail. In depth. A vague answer is a red flag. Walk away.
Why testwork on the actual ore decides the route
Generic advice fails here. It just does. Two refractory ores can have the same gold grade. They can behave completely differently in a roaster. One may roast clean at a relatively low temperature. Easy. Another may sinter into a brick if the temperature overshoots. Disaster. You need testwork on your own drill core or bulk sample. No shortcuts. Start with chemical and mineralogical analysis. That's step one. Then run roasting tests at laboratory scale. Follow with cyanide leach tests on the calcine. The aim is to find the combination of particle size, temperature, oxygen and time. That gives acceptable extraction. You don't want a sticky or sintered product. Trust me.
This is where gold ore testing earns its keep. You'll also want to check the behaviour of arsenic and mercury during roasting. That drives the gas cleaning design. If the ore is variable, test multiple composites. Not just one. One sample from a single drill hole won't tell you how the whole deposit behaves. It can't. The testwork you do now prevents a very expensive mistake in the flowsheet later. Think about that.
From roasting testwork to plant design
Scale-up from a laboratory muffle furnace to a commercial roaster is not linear. Not at all. A lab test tells you whether roasting works. Yes or no. A pilot campaign tells you how it behaves in continuous service. That's different. The design team needs to settle the roaster type, likely a fluidised bed or a two-stage fluidised bed for arsenical ores, and then integrate it with downstream CIL or CIP. The roaster gas handling must connect to the acid plant or scrubber. No leaks. The calcine quench, grinding and cyanidation circuit all have to match the roaster capacity. Perfectly. You can see how the leaching side fits in our gold CIL plant page.
That integration is where a full EPC contractor earns its keep. It's the hard part. Xinhai reports a 15,000 t/d gold processing EPC in Guinea. That's a big one. The company's published figures also include 600+ Mine EPC+M+O projects. And 2,500+ mines served. That's the kind of track record to ask about. When you're interviewing contractors for a roasting plant. Ask to see the process flow diagrams, the mass balance and the equipment list. All three. Ask who will own the process guarantee, if any. Get it in writing. And ask how the roaster supplier will support commissioning. Don't skip that. Roasting is not the sort of unit operation you want to learn on the job. You really don't.
Frequently asked questions
What is the gold roasting process?
Gold roasting is an oxidative pretreatment. It heats refractory gold ore in a controlled atmosphere. Sulphide minerals like pyrite and arsenopyrite react with oxygen. They form porous iron oxides. Organic carbon burns off. It's gone. The resulting calcine is then suitable for cyanide leaching. That's the goal. It's a liberation step. Not a recovery step.
What are the main gold roasting techniques?
The main industrial techniques are whole-ore roasting and flotation concentrate roasting. Two options. Whole-ore roasting treats the entire crushed ore. Everything. Concentrate roasting first floats the sulphides. Then it roasts a smaller mass. Roasters are commonly fluidised bed units. Including two-stage fluidised bed designs for arsenical ores. The choice depends on sulphur grade, arsenic content and heat balance. It's a balance.
What equipment is used in a gold roasting plant?
A roasting plant typically includes the roaster itself. Often a fluidised bed or two-stage fluidised bed. Plus feed preparation, gas cleaning equipment like cyclones, scrubbers and electrostatic precipitators. And calcine handling and quench systems. Downstream, the calcine goes to grinding and a gold leaching circuit. Usually CIL or CIP.
Why is roasting used for refractory gold ore?
Refractory gold ore often contains gold locked inside sulphide minerals. It's trapped. Double-refractory ore also contains carbonaceous matter. That preg-robs dissolved gold. Roasting oxidises the sulphides to expose the gold. It also burns off the carbon. That makes the ore amenable to standard cyanidation. Finally.